





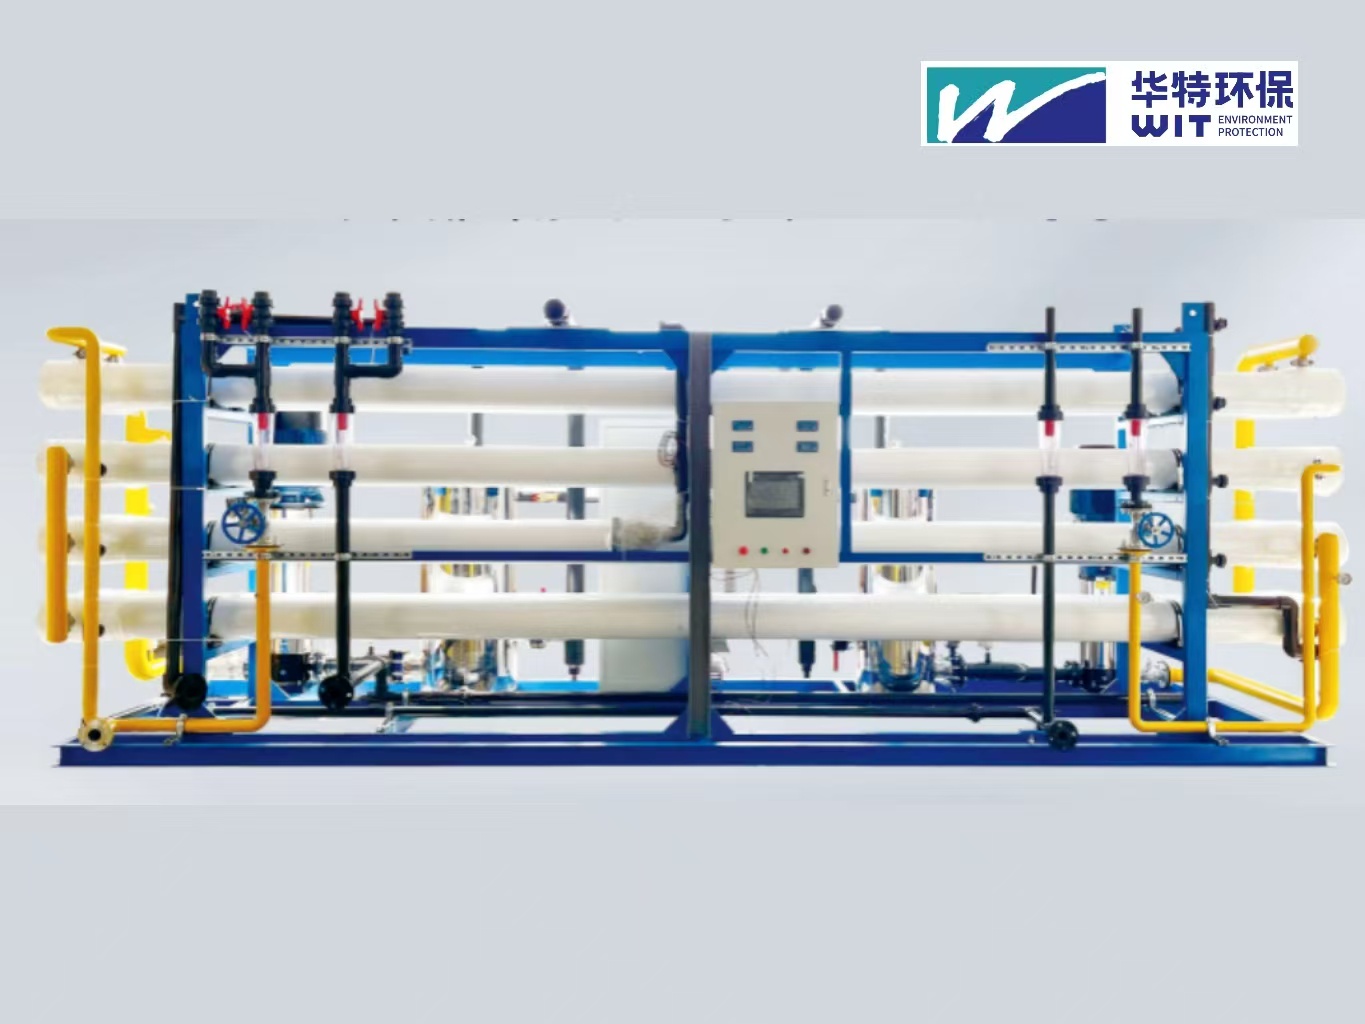
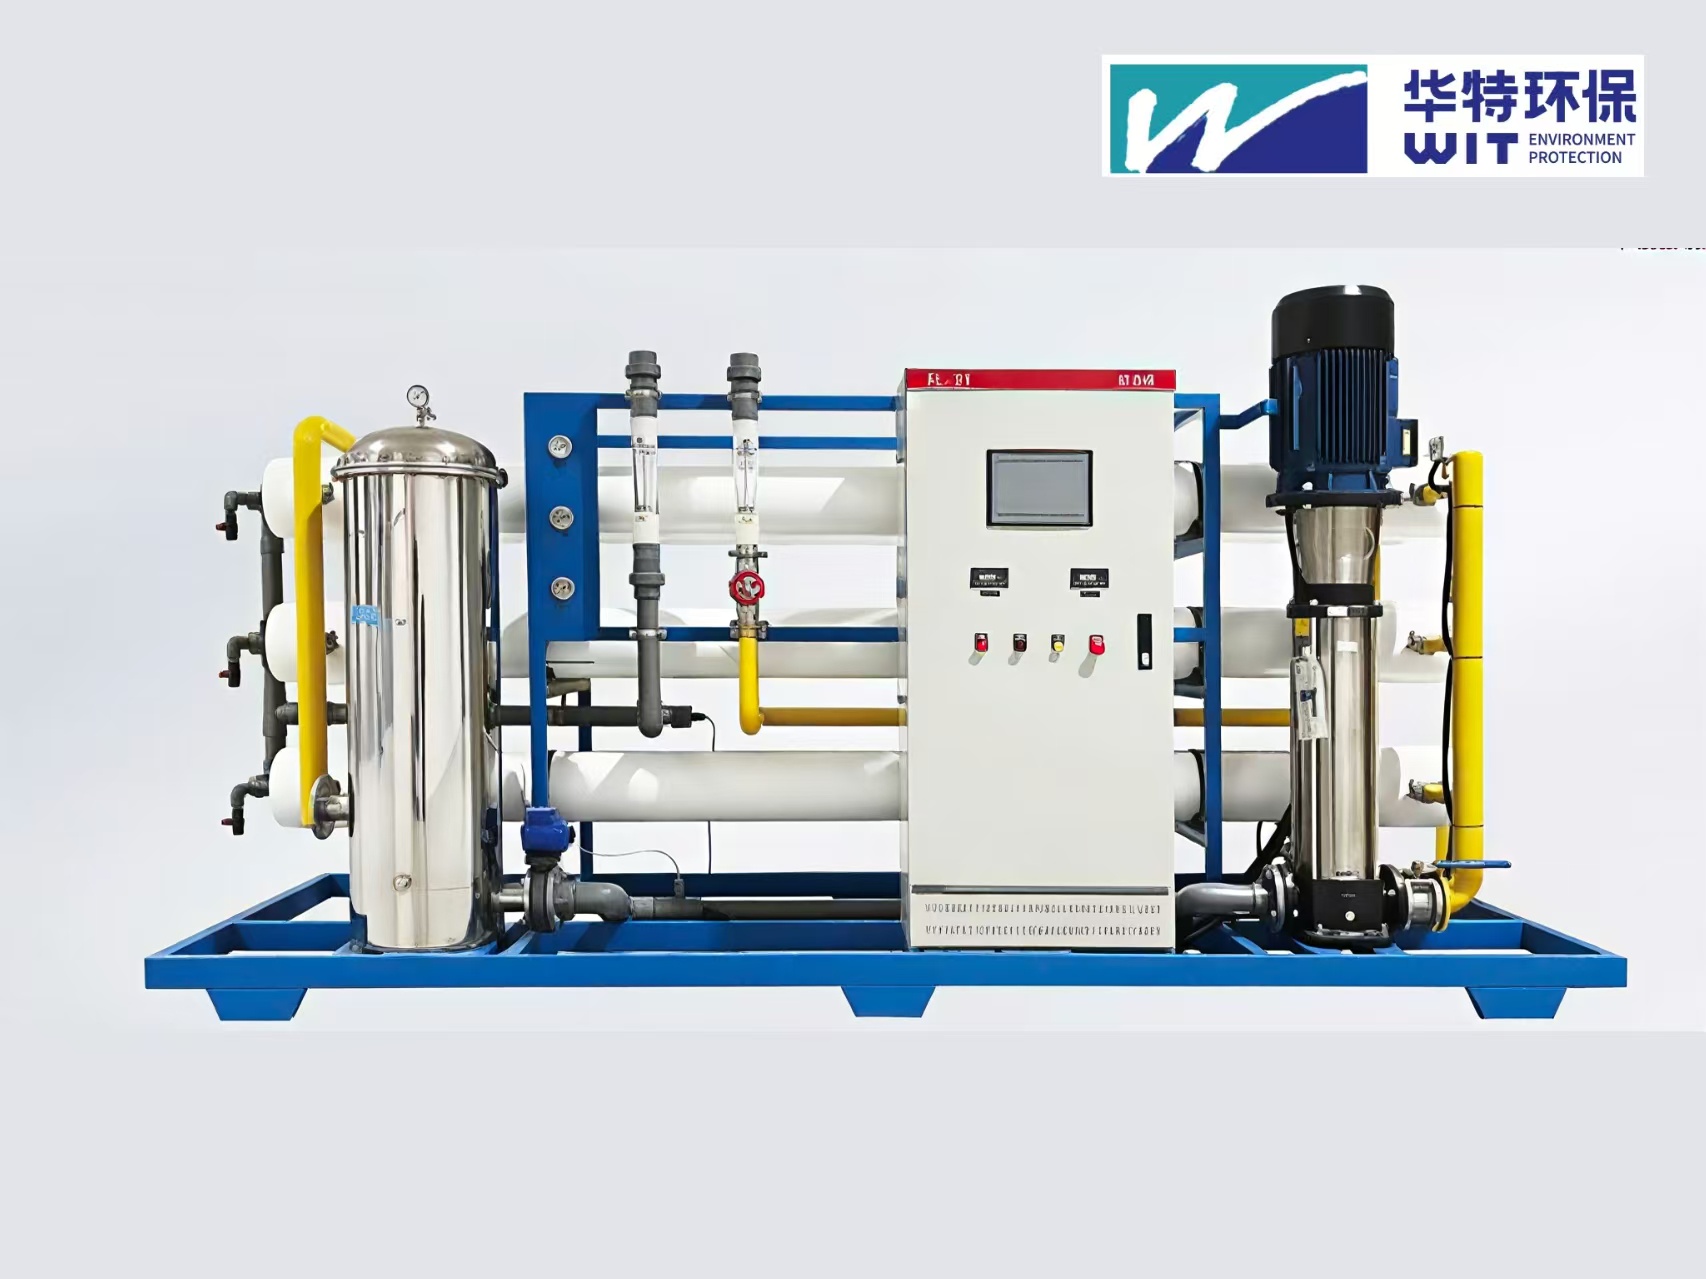
Large-Scale Integrated Skid-Mounted Water Purification Treatment Equipment
Shandong WIT Environment Protection Technique Co., Ltd – 10 Years of Manufacturing Experience in Water Treatment Equipment
Product Introduction
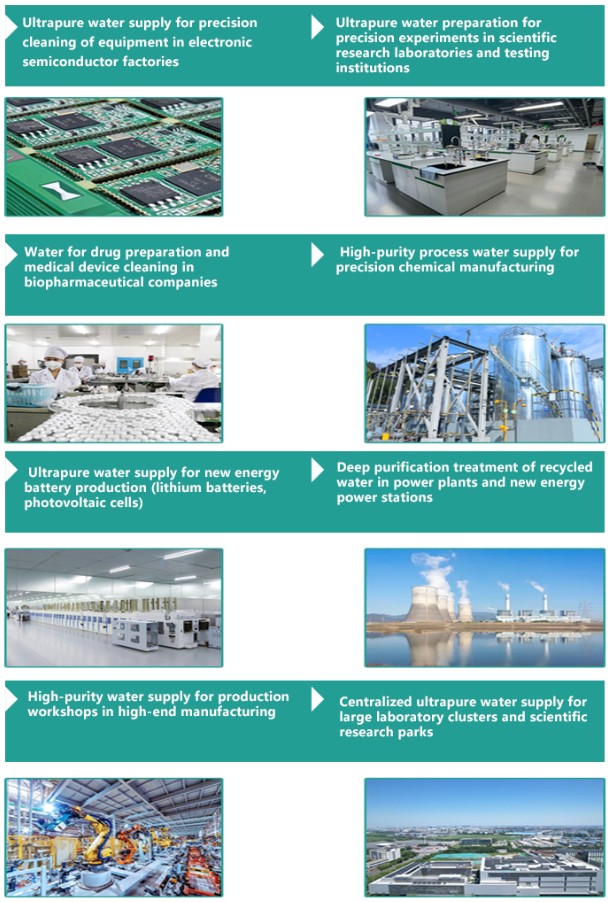
Our self-developed and self-manufactured large integrated skid-mounted water purification treatment equipment is tailor-made for high-end water consumption scenarios including operation & maintenance of electronic semiconductor facilities, precision laboratory research, biopharmaceutical supporting production, fine chemical manufacturing, and new energy battery manufacturing.
Centered on the core objectives of high-yield ultrapure water and easy integrated on-site deployment, the equipment can stably produce ultrapure water with resistivity≥18MΩ·cm and TOC≤50 ppb, fully complying with strict water quality standards for high-end manufacturing processes.
Adopting integrated and modular design, it perfectly fits construction projects with limited site space, stringent water quality requirements and convenient operation & maintenance demands, delivering reliable ultrapure water supply for all high-end water utilization processes.
Core Technology
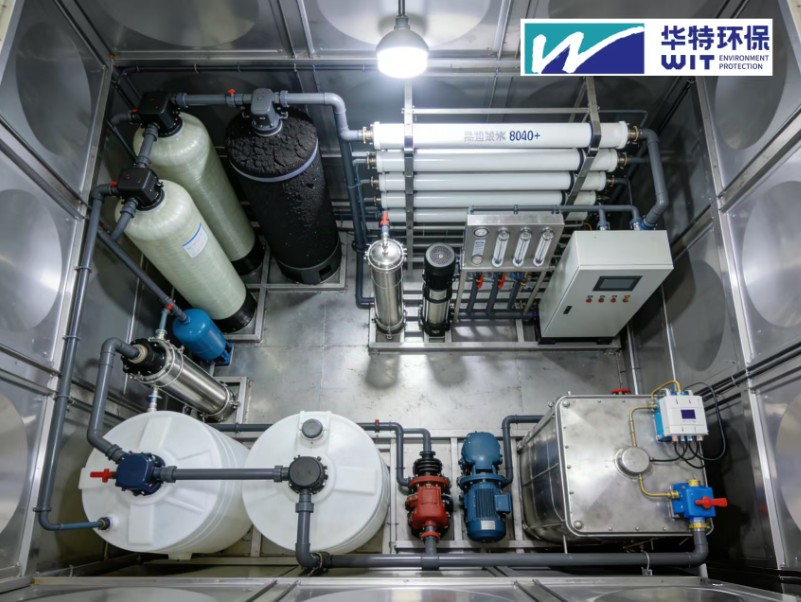
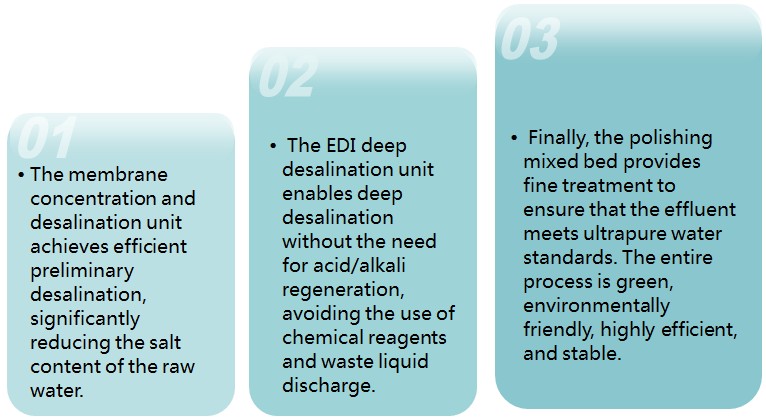
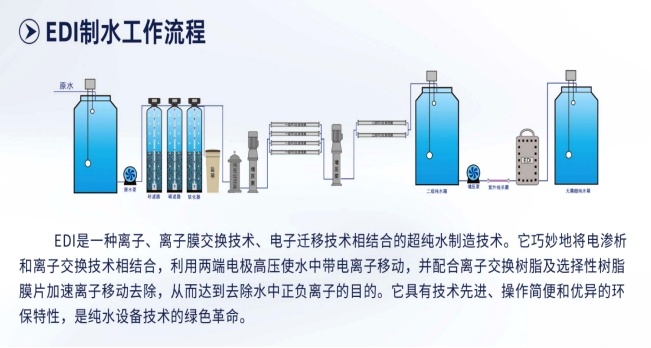
The system adopts a fully integrated full-process technological chain: Pretreatment → Single/Multi-stage membrane concentration & desalination → EDI advanced desalination → Polishing mixed bed.
Its core technical system consists of membrane concentration combined with EDI technology.
The pretreatment unit specially removes impurities such as suspended solids, colloids, residual chlorine and organic matters in raw water to ensure stable operation of the subsequent membrane system and EDI system.
Application Scenarios
Equipment Advantages
1.Ultra-high effluent quality to meet high-end demands
Stably produces ultrapure water with resistivity ≥18 MΩ·cm and TOC ≤50 ppb. Some customized solutions can achieve resistivity >18 MΩ·cm, fully meeting the water quality standards for high-end applications such as electronic semiconductor cleaning, laboratory precision testing, and biopharmaceutical preparation, with stable and consistent water quality.
2. Flexible inlet water requirements with strong adaptability
Can directly treat municipal tap water or softened water (TDS 50–500 mg/L). For project sites, no additional raw water pretreatment system is required—direct connection to the municipal water supply is sufficient, significantly reducing initial infrastructure investment.
3. Small footprint for space-limited sites
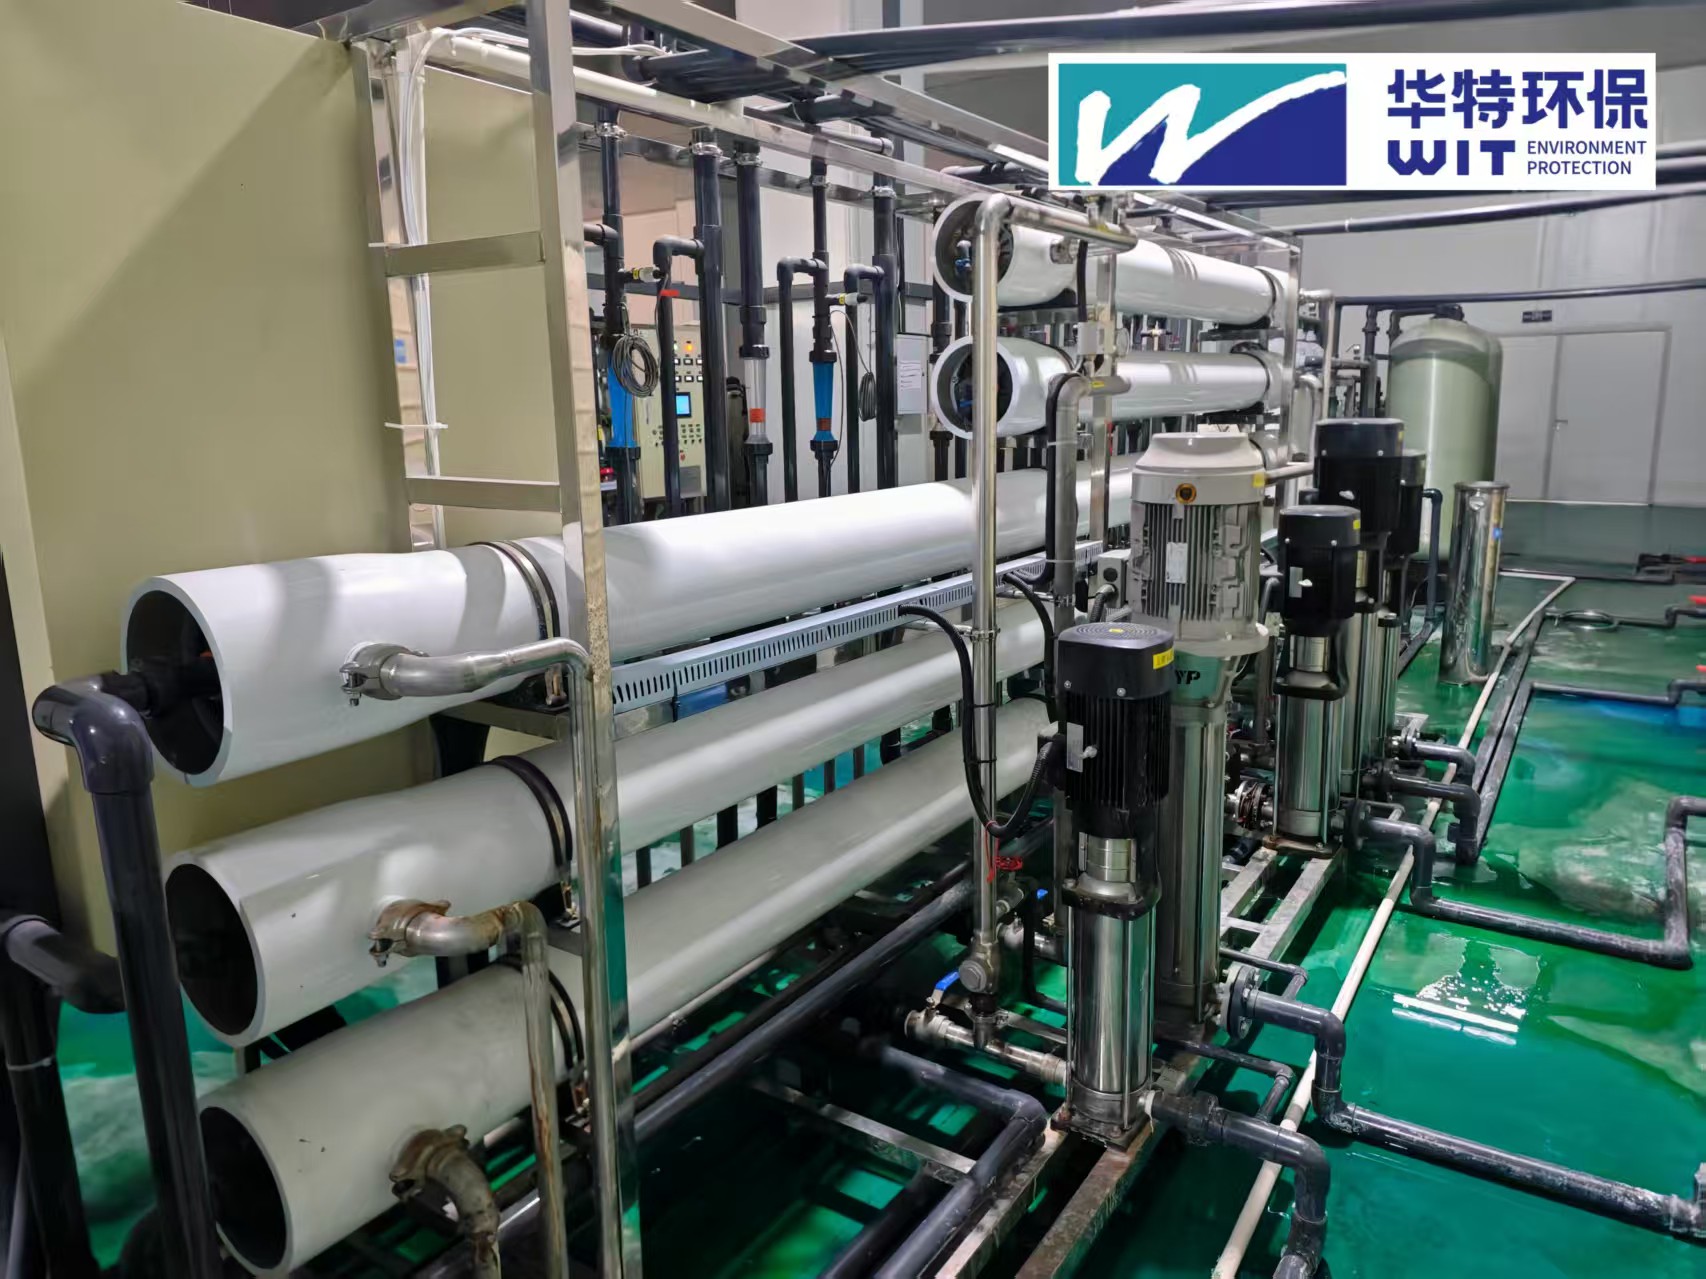
Utilizes a skid-mounted integrated design that highly consolidates multiple treatment units into a compact structure, reducing the footprint by more than 50% compared to traditional ultrapure water equipment. It can be flexibly placed in equipment rooms or laboratory areas of project sites without requiring large dedicated spaces.
4. Extremely short installation cycle, aligning with project timelines:
The equipment is fully pre-assembled and tested at the factory. On-site installation only requires water and electrical connections and pipeline hookups, with completion and commissioning within 1–2 weeks, quickly meeting the high-end water demands of project sites without delaying the overall schedule.
5. Very low operating cost, green and environmentally friendly:
The EDI module requires no acid/alkali regeneration, resulting in zero chemical costs. The modular energy-saving design achieves energy consumption per ton of water far lower than that of traditional equipment. Fully automated operation reduces manual monitoring costs, keeping overall operation and maintenance expenses可控. Additionally, the equipment produces no acid/alkali waste liquid—only a small amount of concentrated water that can be recycled—fully aligning with the principles of green construction and environmentally friendly production.
6. Convenient operation and maintenance, robust technical support:
All equipment components are standardized with a regular structure, making routine maintenance and part replacement easy. Supports remote fault diagnosis and real-time operation monitoring. Staff can monitor equipment status and promptly troubleshoot issues via online systems, lowering the threshold for on-site operation and maintenance.
7. High degree of customization, adapting to all requirements:
The process scheme can be adjusted based on actual ultrapure water quality requirements (resistivity, TOC, etc.). Equipment dimensions and treatment capacity can be flexibly tailored to actual water consumption. The maximum treatment capacity of a single unit reaches 240 m³/day, and multiple units can be combined to meet large-volume demands.
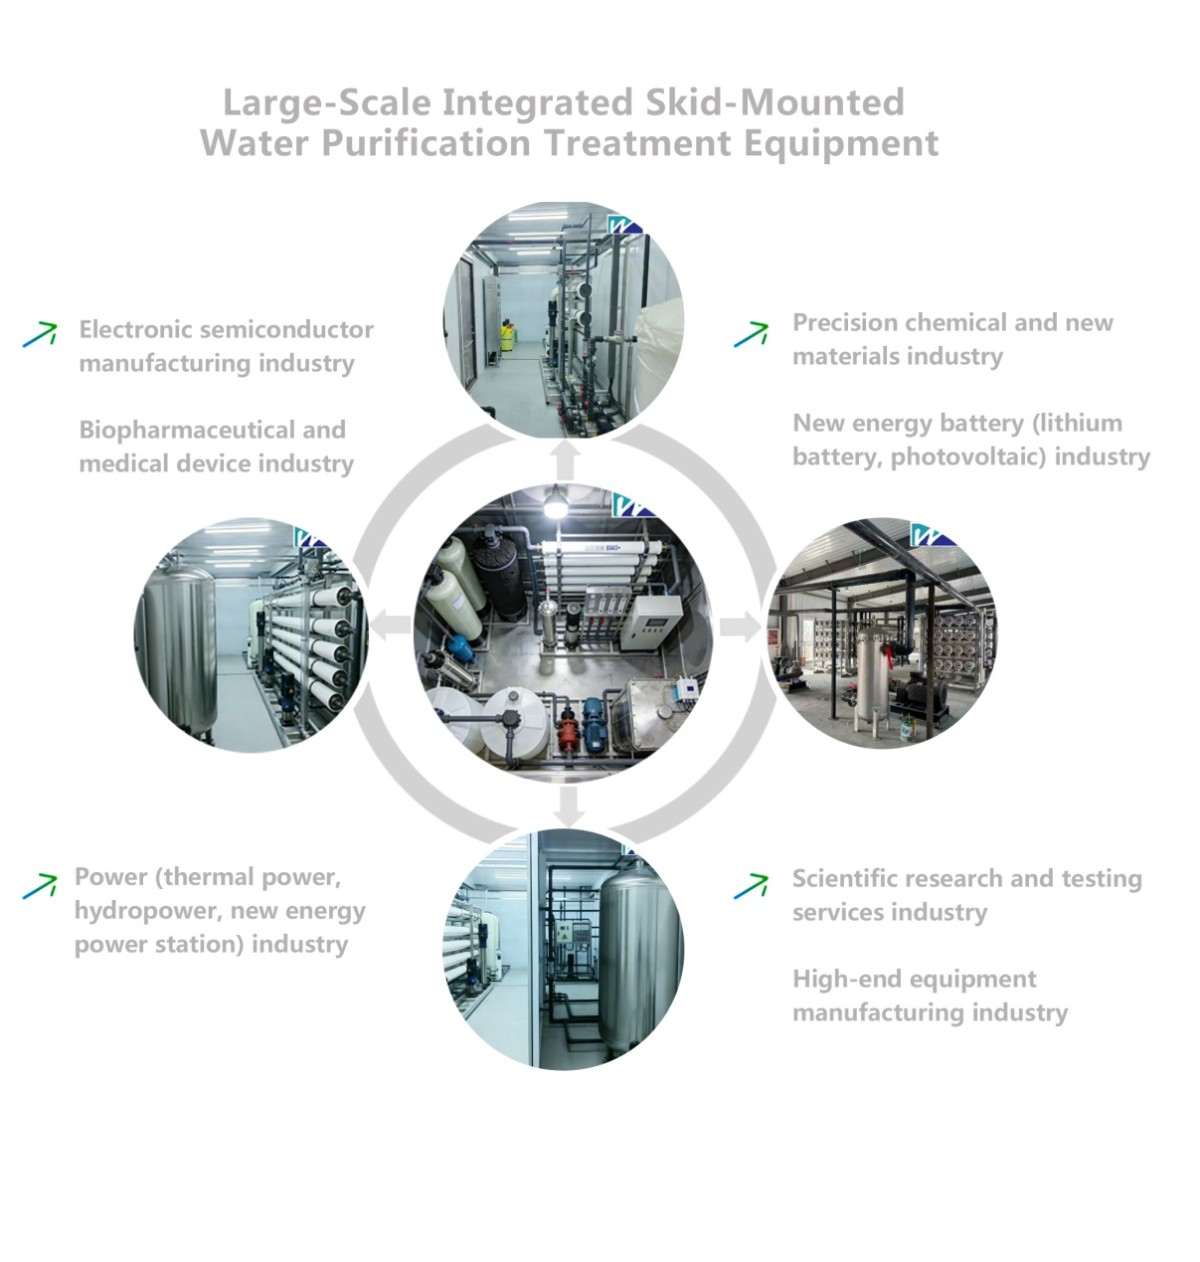
Classic Cases
Ultrapure Water Supporting Project for an Electronic Semiconductor Factory:
Equipping a large-scale electronic semiconductor factory with a skid-mounted water purification system (50-100 m³/d capacity) to stably produce ultrapure water with a resistivity ≥18 MΩ·cm. This meets the water requirements for core processes such as semiconductor chip cleaning and packaging. The integrated design adapts to workshop space limitations, and installation and commissioning were completed within one week.
Purified Water Project for a Biopharmaceutical Company:
Customizing ultrapure water solutions for biopharmaceutical companies, with a capacity of 30-80 m³/d. Utilizing EDI deep desalination technology, there is no acid or alkali wastewater discharge. The effluent TOC ≤50 ppb meets pharmaceutical GMP standards. The entire process is automated, reducing manual maintenance costs.
Water Supply Project for New Energy Lithium Battery Production:
Providing a lithium battery production base with multiple 100-240 m³/d large-scale water purification units. Combined operation meets high-volume ultrapure water requirements, removing heavy metals, impurities, and organic matter from the water to ensure the quality of lithium battery electrodes and electrolytes. This project is compatible with the project's timeline requirements.
Centralized Ultrapure Water Supply Project for a Research Park:
A centralized ultrapure water supply system was built for a provincial-level research park. Each unit has a processing capacity of 80 m³/d, simultaneously meeting the precision experimental water needs of multiple laboratories and R&D centers within the park. It supports remote monitoring and fault diagnosis, and is convenient and efficient to operate and maintain.
Deep Purification Project for Reclaimed Water from a Power Plant:
A large-scale skid-mounted water purification system was provided to a thermal power plant to treat its reclaimed water. Through a fully integrated process, the reclaimed water is purified to ultrapure water standards for use in boiler feedwater and equipment cleaning, achieving water resource recycling and reducing the company's water costs.
Our Commitment
As a professional service provider with over a decade of in-depth experience in water pollution treatment, we consistently pursue technological innovation. Adhering to the service philosophy of "Premium Service & Professional Assurance", we have formulated five-star after-sales service standards to ensure customers can operate our water treatment products efficiently.
If you are confronted with wastewater treatment challenges, please feel free to contact us. We provide free technical consultation and customized solution design to help you select the optimal solution tailored to your needs.
Official Website:https://www.sd-wit-tec.com
E-mail:htwit@sd-wit-tec.com
Service Hotline:0531-85198960


 How to spot poor fabrication quality from chemical dosing skid manufacturers
 When local chemical dosing skid manufacturers are better than overseas suppliers
 Common membrane fouling causes in industrial pure water equipment
 What to check before buying industrial pure water equipment for a new plant
 How ultrapure water equipment helps reduce scaling in dosing systems
 When does industrial pure water equipment become necessary in pulp bleaching
GET A FREE QUOTE
Service Commitment: Upon receipt of your message, a dedicated representative will contact you as soon as possible to provide efficient and professional service support.
